How to specify stainless steel profiles for tight-tolerance fabrication
How to Specify Stainless Steel Profiles for Tight-Tolerance Fabrication
For procurement teams sourcing precision components, specifying Stainless Steel Profiles correctly is one of the most effective ways to control quality, cost, and delivery risk. Tight-tolerance fabrication is not solved by writing “stainless steel, to drawing” on a purchase order. A supplier still needs to know which dimensions are functionally critical, how straight the profile must be, what surface condition is acceptable, how material identity will be verified, and which inspection records must travel with the shipment.
The practical challenge is that a profile can look simple while carrying several layers of variation. A flat bar may have acceptable width and thickness but still bow after cutting. A custom channel may meet its external dimensions yet have an inconsistent internal radius that prevents a mating part from seating correctly. A polished architectural section may be dimensionally sound but rejected because the protective film trapped moisture or adhesive residue. These are not unusual supplier failures; they are usually gaps in the original specification.
A workable specification should help the supplier quote the right production route from the beginning. It should also help the buyer avoid paying for precision where it has no functional value. The goal is not to demand the tightest tolerance available. It is to define the tolerances that the finished part actually needs.
Start with the fabrication route, not only the profile shape
“Stainless steel profile” covers a wide range of products: flat bar, angle, channel, tee, solid special sections, hollow sections, laser-welded shapes, roll-formed sections, and cold-drawn profiles. Two suppliers may offer the same nominal geometry but make it by entirely different routes. That matters because the route affects achievable tolerance, internal stress, surface finish, lead time, and the amount of machining or straightening required later.
Cold drawing can be appropriate where dimensional consistency and a cleaner surface are important. Roll forming often makes sense for long, lighter-gauge open sections, but springback and profile twist must be considered. Laser-welded profiles allow more complex geometries and can reduce material waste compared with machining from solid stock; however, weld location, heat tint, distortion, and post-weld finishing become part of the requirement. Hot-rolled sections are often economical for less demanding structural work, but they should not be assumed suitable for close-fit assemblies without downstream processing.
This is why a drawing should not simply copy a catalog size and add a tight overall tolerance. If the profile will be machined after receipt, the procurement team should ask whether the supplied dimensions are intended as finished dimensions or machining allowance. Confusing the two creates a familiar dispute: the supplier believes it delivered oversize stock for finishing, while the buyer expected a ready-to-use precision profile.
Define material in a way that matches the service environment
Grade selection should be linked to the actual exposure, fabrication method, and joining process. For many general indoor applications, a commonly used austenitic stainless grade may be sufficient. Where chloride exposure, washdown conditions, coastal atmospheres, or certain chemical environments are involved, a more corrosion-resistant grade may be necessary. The exact decision depends on temperature, concentration, crevice conditions, cleaning chemicals, and whether the surface will be scratched or welded in service.
A grade name alone is often incomplete. Buyers should state the governing material designation system required by the project, such as an ASTM, EN, JIS, or other agreed specification, rather than assuming equivalent names will be interpreted identically. If dual certification is acceptable, say so. If it is not acceptable, make that clear before quotation. “Equivalent grade” is a commercial phrase, not a complete technical requirement.
For tight-tolerance fabrication, material condition can matter as much as alloy grade. Cold-worked material may offer higher strength but can be less forgiving during bending. Annealed material may form more predictably but may not meet a strength requirement without a design adjustment. If magnetic response, low-temperature toughness, weldability, or controlled hardness is relevant, it belongs in the specification. Do not leave these points to a generic mill standard unless that standard has been reviewed against the application.
Request traceability at the right level
For critical fabricated parts, it is reasonable to request a material test certificate with heat or cast traceability, commonly referred to in many supply chains as an EN 10204 Type 3.1 certificate. Whether this is needed for every order depends on the consequence of material substitution. A decorative trim component and a profile used in a pressure-related assembly should not necessarily carry the same documentation burden.
The important detail is continuity. If long lengths are cut into shorter pieces, labels and records need to preserve the relationship between each supplied batch and its certificate. A certificate that identifies the original coil or bar is of limited value if the delivered profiles cannot be tied back to it. This becomes especially relevant when material is split across several production lots or when the supplier performs additional fabrication.
Put tolerances where the assembly needs them
The most expensive stainless profile is often not the one with the highest unit price. It is the one that causes sorting, rework, fixture adjustments, delayed assembly, or a last-minute airfreight replacement. Yet applying a blanket tolerance to every dimension is not a sensible cure. Tight tolerances should be assigned based on function.
Separate dimensions into three groups: critical interfaces, controlled but non-critical features, and reference dimensions. Critical interfaces include features that locate the part, create a seal, guide movement, or mate with another component. These need clear limits and a stated measurement method. Controlled non-critical features may need reasonable consistency for appearance or process stability, but they can often use the supplier’s standard capability. Reference dimensions should not accidentally become inspection obligations.
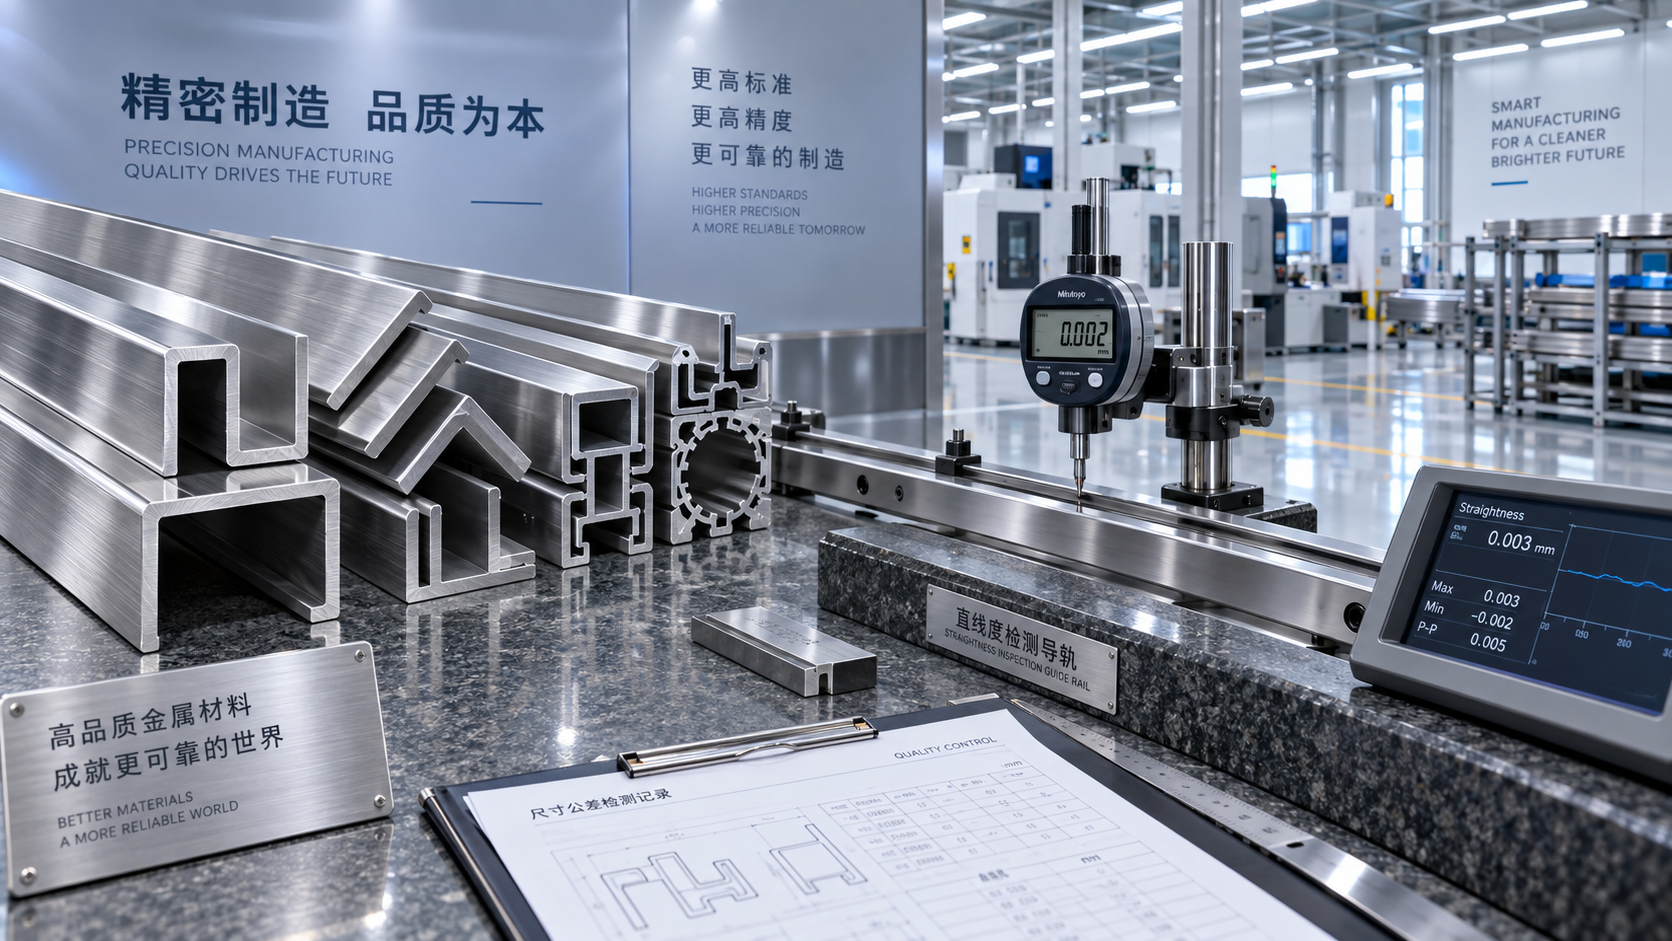
Straightness deserves particular attention. It should be expressed over a defined length, not just as a vague statement that the material must be “free from distortion.” Long profiles naturally magnify small deviations. A tolerance that is workable on a short cut piece may be difficult or costly on a full production length. Specify whether the requirement applies before or after cutting, because residual stress can be released when long stock is cut into shorter parts.
For complex profiles, use clearly identified datums on the drawing. If a profile’s internal slot is the functional feature, dimensioning from an outside face may create unnecessary variation at the point that matters. Geometric tolerancing can be useful, but only when both parties understand how it will be inspected. A profile manufacturer may measure cross-section with gauges, optical equipment, or coordinate measurement methods; the selected method and sampling approach should be agreed when tolerances are particularly close.
Surface finish is a functional requirement, not a cosmetic footnote
Stainless steel is often chosen for appearance and corrosion resistance, but surface finish affects more than appearance. Rougher surfaces can retain contaminants more readily. Grinding marks may be unacceptable on visible assemblies. Heat tint beside welds can reduce corrosion resistance if it is not properly addressed. A profile that will be bonded, sealed, polished, or used in a hygienic environment needs a finish requirement that reflects the downstream process.
Avoid vague phrases such as “high polish” or “commercial finish.” State the required finish designation where applicable, the direction of grain for visible faces, and which surfaces are cosmetic. If a roughness value is genuinely necessary, identify the test standard or measurement convention agreed for the project. It is also useful to define permissible surface conditions: scratches, roll marks, pits, weld discoloration, edge cracks, or handling marks. Without this, inspection becomes subjective and rejection decisions tend to occur after the material has already reached the production line.
Protective film should be specified only when it serves a real purpose. Film can reduce handling damage on decorative surfaces, but it adds cost and must be compatible with laser cutting, bending, storage time, and removal conditions. Procurement should clarify whether film is required on one face or all visible faces, and whether any adhesive residue is unacceptable.
Make inspection and acceptance practical
An inspection plan should focus on the characteristics that would stop fabrication or impair service. Requiring a full dimensional report on every length may be justified for a highly controlled application, but it is usually excessive for routine production. The better approach is to define the critical characteristics, the inspection frequency, the lot definition, and the documents required at release.
For a first order, a first article sample or pre-production approval can be valuable, especially for a new custom cross-section. It gives both sides a chance to confirm not just dimensions but packaging, labeling, straightness after cutting, and surface appearance. This is often less costly than discovering a drawing interpretation problem after a full batch has been produced.
Receiving inspection should be aligned with the supplier’s controls. If the buyer will check width using a caliper while the supplier releases material using a different method and temperature condition, small disagreements are predictable. For very close dimensions, agree on measurement location, instrument resolution, part conditioning, and whether burrs are included or excluded. Stainless profiles are not immune to measurement variation simply because they are metallic.
Ask for a quote that exposes the real cost drivers
A quote comparison is meaningful only when suppliers are pricing the same technical scope. Provide the profile drawing, material standard, required condition, tolerances, finish, lengths, annual or batch quantities, packaging expectations, documentation, and delivery destination. If the requirement is still under review, identify the open points rather than allowing each supplier to make different assumptions.
Ask suppliers to identify any dimensions or requirements that need special tooling, secondary straightening, machining, sorting, or enhanced inspection. This is not merely a negotiation tactic. It reveals whether a lower unit price is based on standard production capability while another quote includes the controls necessary to meet the intended use.
Length optimization is often overlooked. Ordering profiles in standard mill lengths may reduce material cost, but it can increase internal scrap, cutting time, and handling. Conversely, custom cut lengths can simplify production but introduce a cutting tolerance and potential end-deformation issue. The right choice depends on the nesting yield, the capability of the next process, and freight constraints. Long, polished profiles may also require more robust packaging than short industrial cut pieces; damage in transit can erase any apparent savings from cheaper packing.
A specification checklist that suppliers can actually use
Before releasing a purchase order for precision Stainless Steel Profiles, confirm that the document package answers these questions:
- What exact profile geometry, revision level, and units apply?
- Which material grade, product standard, and material condition are required?
- Which dimensions are critical, and what are the allowed limits?
- How are straightness, twist, bow, cut length, and end squareness controlled?
- Which faces require a defined finish, grain direction, or protective film?
- Are welds permitted, and if so, where may they be located and how must they be finished?
- What material certification, traceability, dimensional records, and first-article approval are needed?
- What packaging prevents damage, contamination, or profile distortion during shipment?
The strongest specifications are specific without being punitive. They define the features that drive fit, function, and appearance, while allowing the manufacturer reasonable freedom in areas that do not affect the finished assembly. If a tolerance is difficult to justify, review the mating-part requirement before placing it on the profile drawing. That conversation, held before quotation rather than after receipt, is usually where the largest cost and delivery risks are removed.
Get real-time quotes
Interested? Leave your contact details.